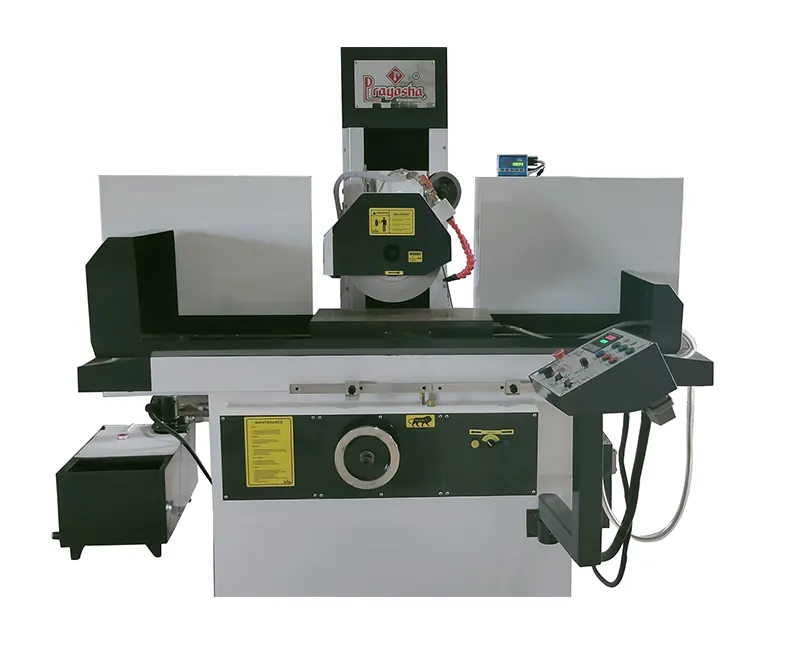
A surface grinding machine is a machine tool that uses a rotating abrasive wheel to make a surface flat, smooth and accurate to size. It is usually the last operation on a part, after milling or turning and often after heat treatment.
Main parts
Base and column
The heavy structure that carries everything. On a column-moving design like Prayosha's, the column carries the wheel head.
Table
Holds the work, usually on a magnetic chuck, and moves back and forth under the wheel.
Wheel head and spindle
Holds and drives the grinding wheel. Spindle bearings decide the finish.
Cross slide
Steps the work across the wheel after each stroke.
Vertical feed
Lowers the wheel by the depth of cut, in steps as fine as 0.002 mm.
Hydraulic and coolant systems
Drive the table, and keep the work and wheel cool and clean.
How it works
- The part is clamped on the magnetic chuck.
- The wheel is dressed and lowered until it just touches the part.
- The table reciprocates while the cross slide steps across after each reversal.
- The wheel is lowered by a small depth for each pass until the part reaches size.
- Spark-out passes, with no extra depth, remove the last spring-back.
Types of surface grinding machine
- Horizontal spindle, reciprocating table: the most common type for precision work
- Hydraulic (oil type): an oil hydraulic table drive
- PLC / automatic: programmable down feed
- CNC: programmed modes, profiles and dressing
- Double column: gantry type for very large work
Read more: functions, applications and advantages.
Frequently asked questions
What is the purpose of a surface grinder?
To produce flat, smooth surfaces held to accurate size, flatness and parallelism.
Is surface grinding done before or after heat treatment?
Usually after, because the abrasive wheel can cut hardened steel that ordinary cutting tools cannot.
What holds the workpiece?
Usually an electro-magnetic chuck for steel parts, or vises and fixtures for others.
